English
 Chemical Industry
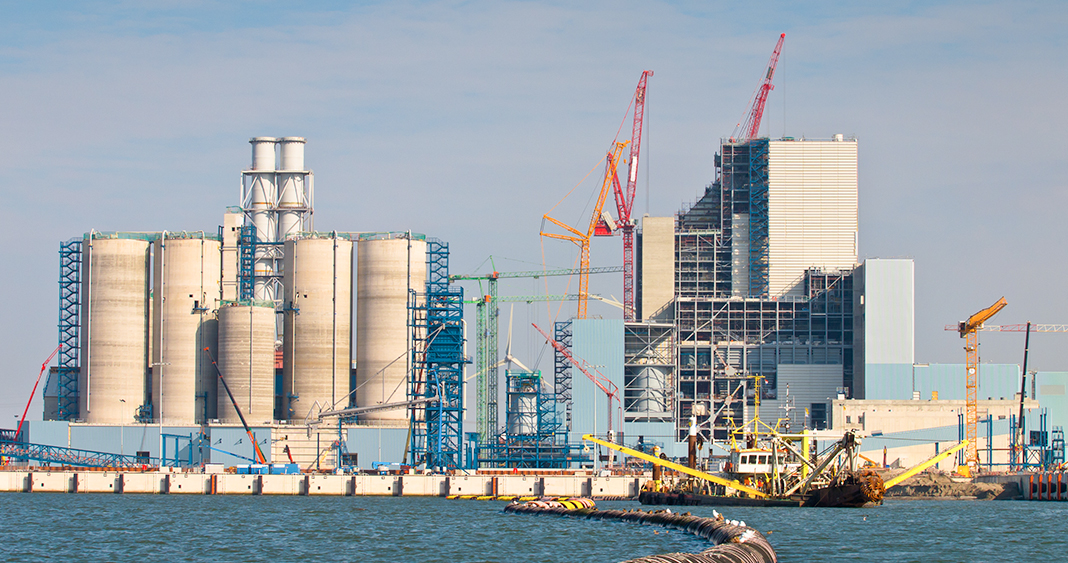
Chemical production environments are filled with highly corrosive chemical media, flammable and explosive gases, and high-temperature and high-pressure conditions, placing high demands on cables for acid and alkali resistance, oil resistance, flame-retardant and explosion-proof performance, and signal interference resistance. Any line failure may cause major safety accidents.
Solutions
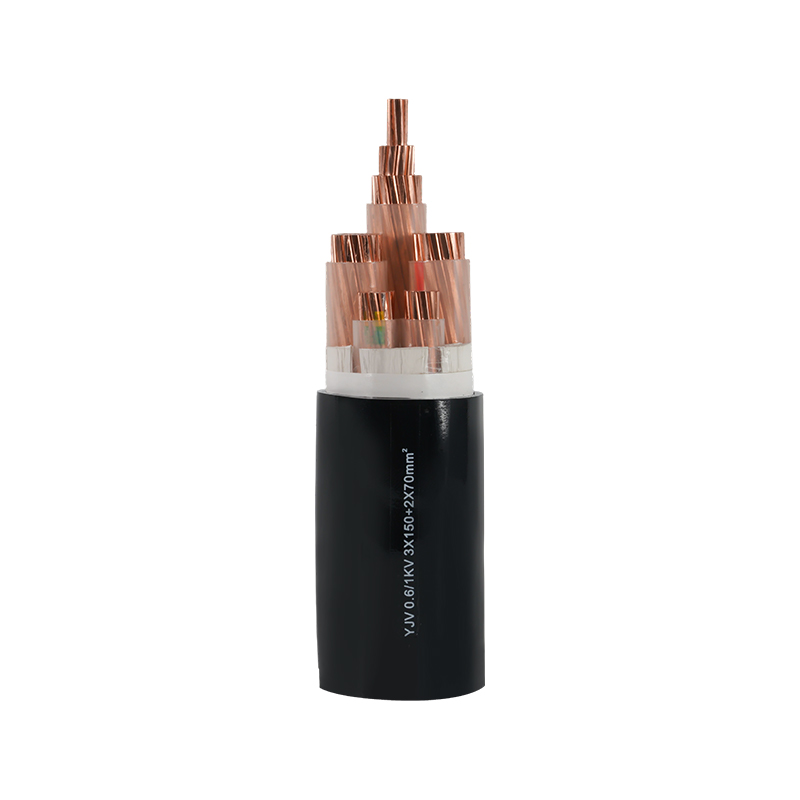
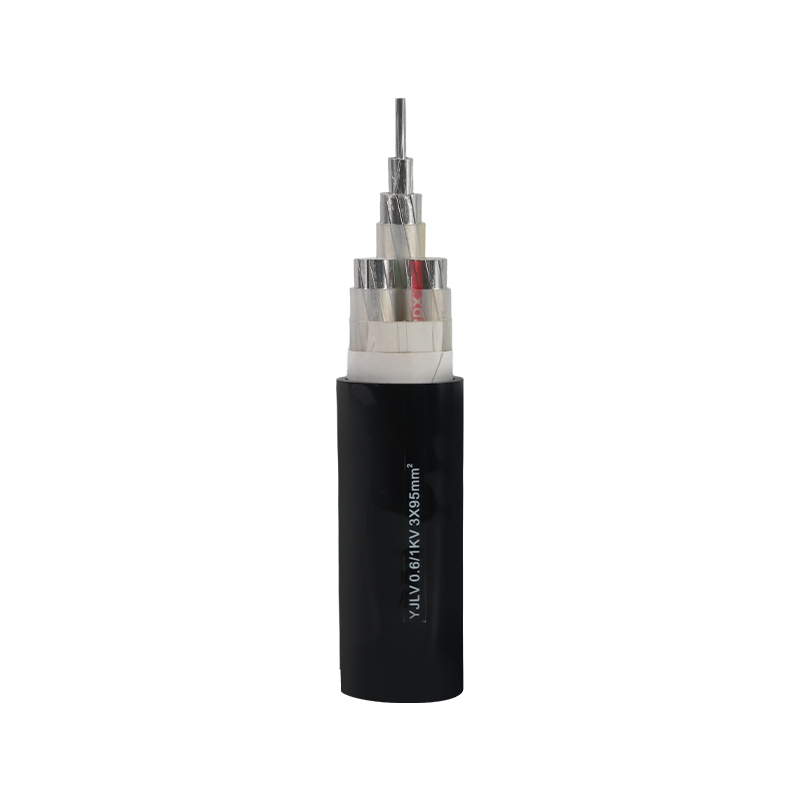
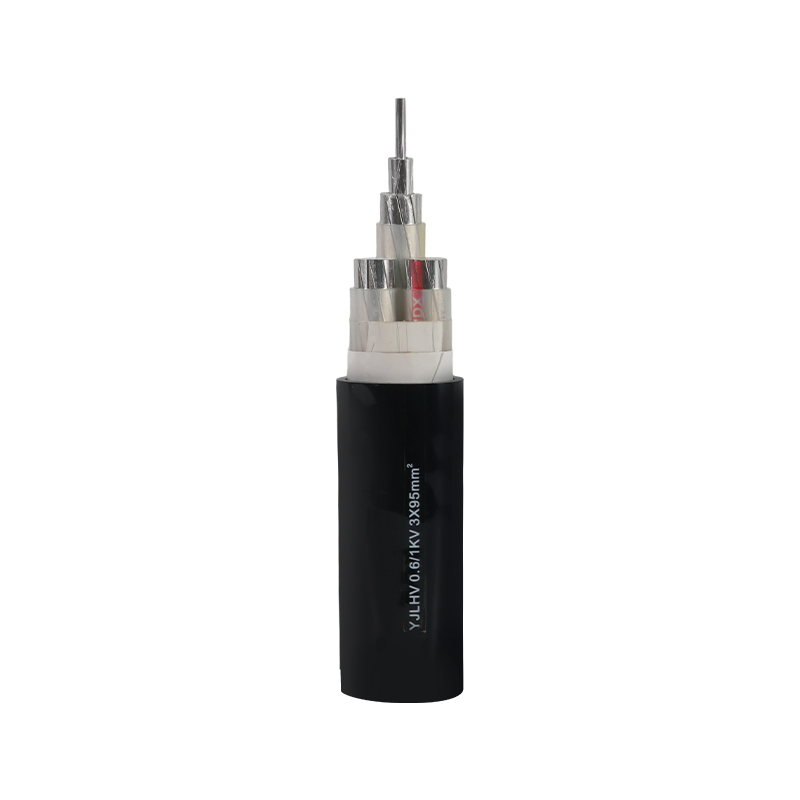
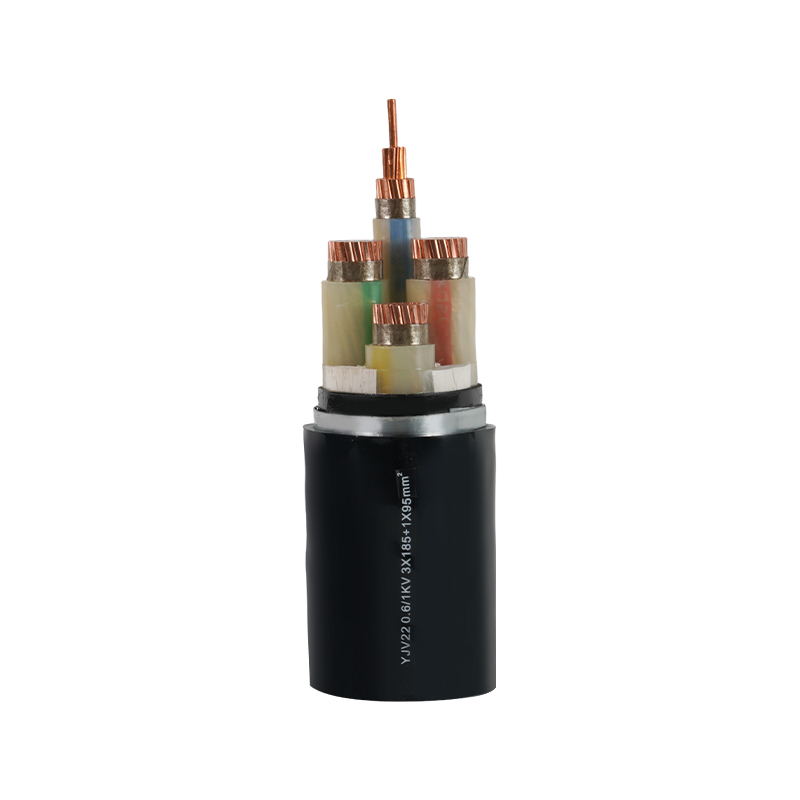
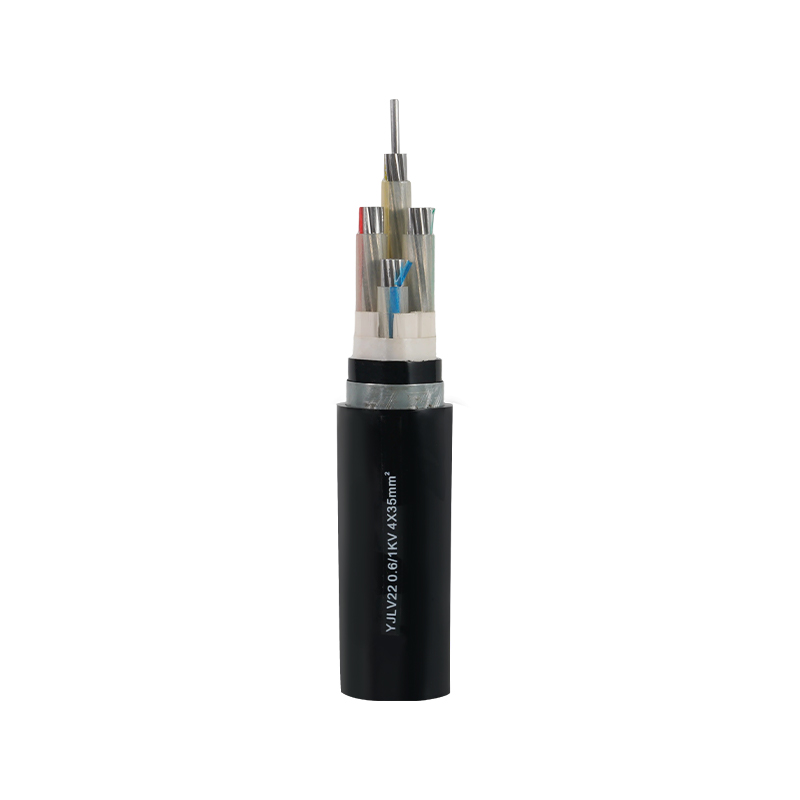
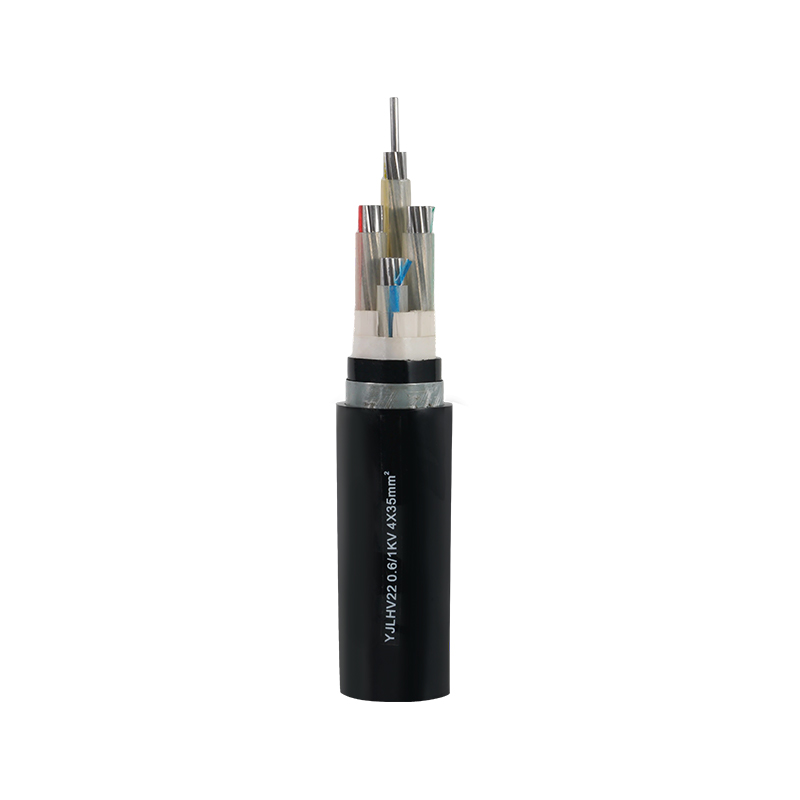
For the harsh environment of chemical zones, low-smoke halogen-free, UV-resistant, and oil-sludge-resistant special sheath materials are used to ensure the sheath does not become brittle or crack over time. For explosion-proof core zones, computer cables and control cables for intrinsically safe circuits are provided, combined with high-density braided shielding to achieve zero-error transmission of instrument signals. Large cross-section cross-linked power cables are also supplied to meet the stable power supply needs of high-load equipment.
Specific Applications
- Reactor power transmission
- Explosion-proof power supply for tank farms
- Pipeline heat tracing power supply
- Fire emergency refractory circuits
- Wastewater treatment equipment power supply
Contact Us
Contact us
-

Tel: +86-510-87201868 / +86-510-87212512
-

Phone: +86-15250829090
-

Fax: +86-510-87208748 / +86-510-87212508
-

Industrial Area A, Guanlin town, Yixing, Jiangsu Province. China.
Copyright @ Jiangsu Dongxu Cable Co. , Ltd. Rights Reserved.